Wheel Hub Bearing Inspection: Build a Plan Buyers Can Verify
A wheel hub bearing inspection plan should connect each requirement to a method, a result and a response when the requirement is not met. Checking appearance alone is insufficient, but asking for every possible test is not a practical alternative. Start with the intended product and application, identify the characteristics that matter, and agree which checks belong at sample approval, production release and receiving.
For distributors and purchasing teams, the goal is a usable acceptance record. It should explain which part was examined, what specification applied, how the checks were performed and what decision followed. This guide provides a framework for discussing that record with suppliers. It does not establish universal limits or claim that any particular factory performs all the tests described.
Define the product and the approval stage
Specify whether the purchase is for a bearing cartridge, a flanged unit, a complete hub assembly or a kit. Include the supplier reference, drawing revision and intended application. A plan for one assembly should not be copied to another simply because both appear under the same wheel hub bearing category.
Then identify the stage of approval. A development sample review may answer whether a proposed design meets agreed requirements. Routine final inspection may check production characteristics. Receiving inspection may confirm delivery identity, condition and selected attributes. These activities can complement each other, but their results should not be presented as equivalent.
For example, a package count and a visual check at a distributor’s warehouse do not demonstrate fatigue performance. Conversely, a development test report does not prove that the correct labels and kit contents arrived in the latest shipment. The plan should make these boundaries visible so each team knows what its acceptance decision actually covers.
Translate requirements into checkable characteristics
Begin with the controlled product definition and the relevant customer requirements. Identify the features that affect fit, function, identification and protection during handling. Use a characteristic identifier that can be traced back to the drawing or specification. Avoid a checklist whose acceptance column merely says “good quality.”
Describe each check at a useful level. “Dimension inspection” is too broad if the shipment can fail because of one particular pilot or mounting face. “ABS test” is ambiguous if the supplied part contains an encoder but no sensor. “Noise passed” is incomplete unless the test conditions and applicable limits are known.
Where a requirement is missing, record a clarification action before inspection. Inspectors should not create tolerances from previous experience with a different part. If the buyer and supplier disagree about a limit, resolve it through the technical approval process and preserve the revision history. Changing the limit after seeing an unfavourable result can hide the actual problem.
| Characteristic | Requirement source | Method information | Recorded outcome |
|---|---|---|---|
| Product identity | Order and approved reference | Label and marking comparison | Matched identity or stated discrepancy |
| Mounting feature | Controlled drawing | Datum, equipment and contact location | Value, unit and decision |
| Rotational characteristic | Applicable test specification | Fixture and operating conditions | Result against the specified limit |
| Sensing function | Encoder or sensor specification | Compatible test arrangement | Result and scope of the check |
| Kit contents | Approved packing list | Item-by-item comparison | Count and missing or incorrect items |
| Packaging condition | Agreed packing specification | Visual and other agreed checks | Condition and disposition |
Control identity before measuring anything
An excellent measurement report is of limited value if it cannot be connected to the delivered product. Identify the sample, lot, supplier reference and drawing revision before testing. Preserve the package label or its photograph. Where several similar references are examined at once, use physical separation and clear temporary identification.
Traceability should continue through the inspection activity. If a sample is moved to a laboratory or a specialist test station, its identity must remain connected to the request and result. Avoid sending unlabelled parts with a spreadsheet that lists several possible numbers. The receiving laboratory should not have to infer which sample belongs to which row.
The automotive bearing traceability guide discusses the wider record chain. For an inspection plan, a practical rule is simple: another authorised person should be able to locate the relevant result from the order and lot identifiers without relying on the original inspector’s memory.
Make dimensional checks repeatable
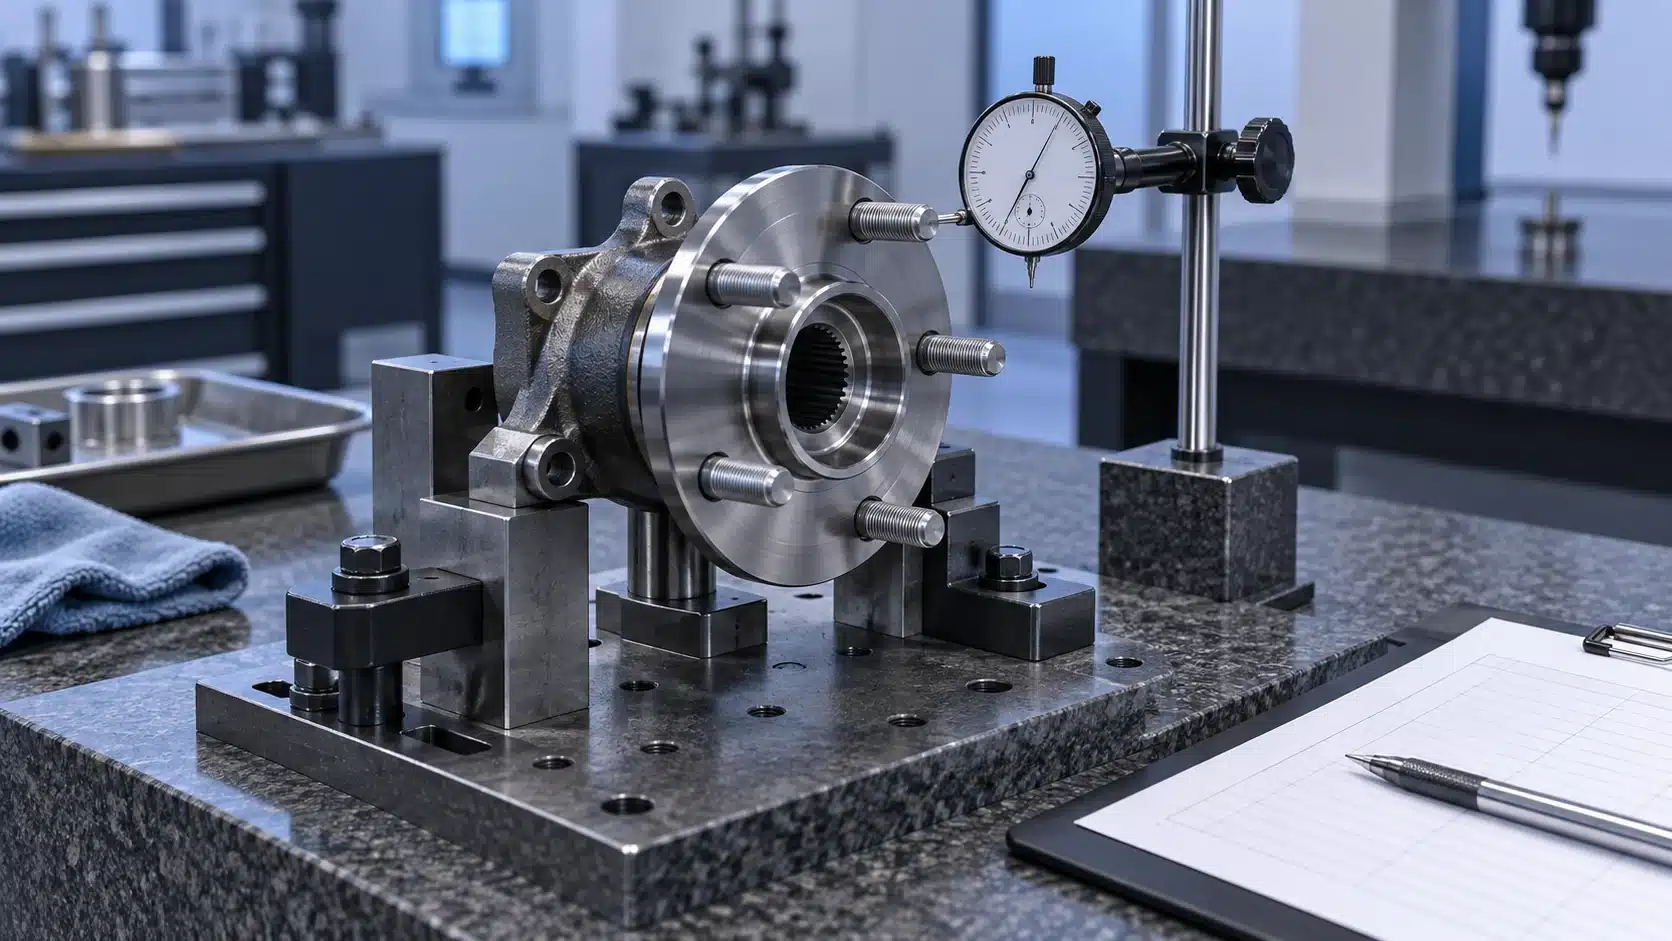
Specify the datum references and measurement locations for each important feature. A flange height is not adequately defined until the two relevant faces are named. A pilot diameter should identify the actual cylindrical land rather than a nearby chamfer. Use the flange dimension guide to clarify these terms before the inspection sheet is issued.
Choose equipment and fixturing suitable for the measurement task. Calibration is necessary where applicable, but the setup, operator technique and environmental conditions can also influence the result. NIST’s discussion of CMM traceability and uncertainty explains why task-specific measurement factors matter alongside instrument calibration.
Record measured values when the decision benefits from them, rather than keeping only a pass mark. Values help investigate drift, compare methods and understand a disputed result. Define how results near an acceptance boundary will be handled. The responsible quality team should establish the decision rule; a buyer should not invent one after delivery.
Treat runout and rotation as specified tests
Runout, rotational torque, clearance and preload describe different characteristics. Their interpretation depends on the product design and measurement arrangement. A hand-spin impression is not interchangeable with a controlled test, and a dial indicator placed near a hub does not by itself define a valid runout measurement.
Ask for the fixture, reference surfaces and loading or clamping conditions used by the applicable method. If a torque or movement characteristic is checked, the method should identify the conditions that affect it. A sealed assembly’s behaviour should be evaluated against its own requirements rather than a general expectation that every bearing must spin freely for a long time.
Where a shop-floor check is intentionally qualitative, name it accurately. It can be useful to screen for obvious damage or an unusual condition, but it should not be reported as a quantitative performance test. Escalate an uncertain result through the agreed reaction plan instead of repeating the same informal check until someone feels reassured.
Define noise, vibration and ABS checks separately
A noise or vibration result requires a defined method, sample identity and acceptance basis. Ask which operating conditions were used and how the signal was evaluated. Results from different fixtures or conditions should not be compared as if they were produced by the same method. Avoid specifying a universal limit across unrelated hub families.
For ABS-related checks, distinguish encoder presence and orientation from functional compatibility. The encoder specification article explains that a viewing aid and a functional test answer different questions. If a sensor is included, confirm that the test scope covers the supplied configuration rather than a different reference arrangement.
Do not state that every delivered bearing was road-tested because one sample was evaluated. Record the actual scope: which units, which conditions and which criteria. That wording protects the usefulness of the evidence. A narrow, accurate result is more valuable than a broad statement that the underlying test cannot support.
Include seals, protection and kit contents
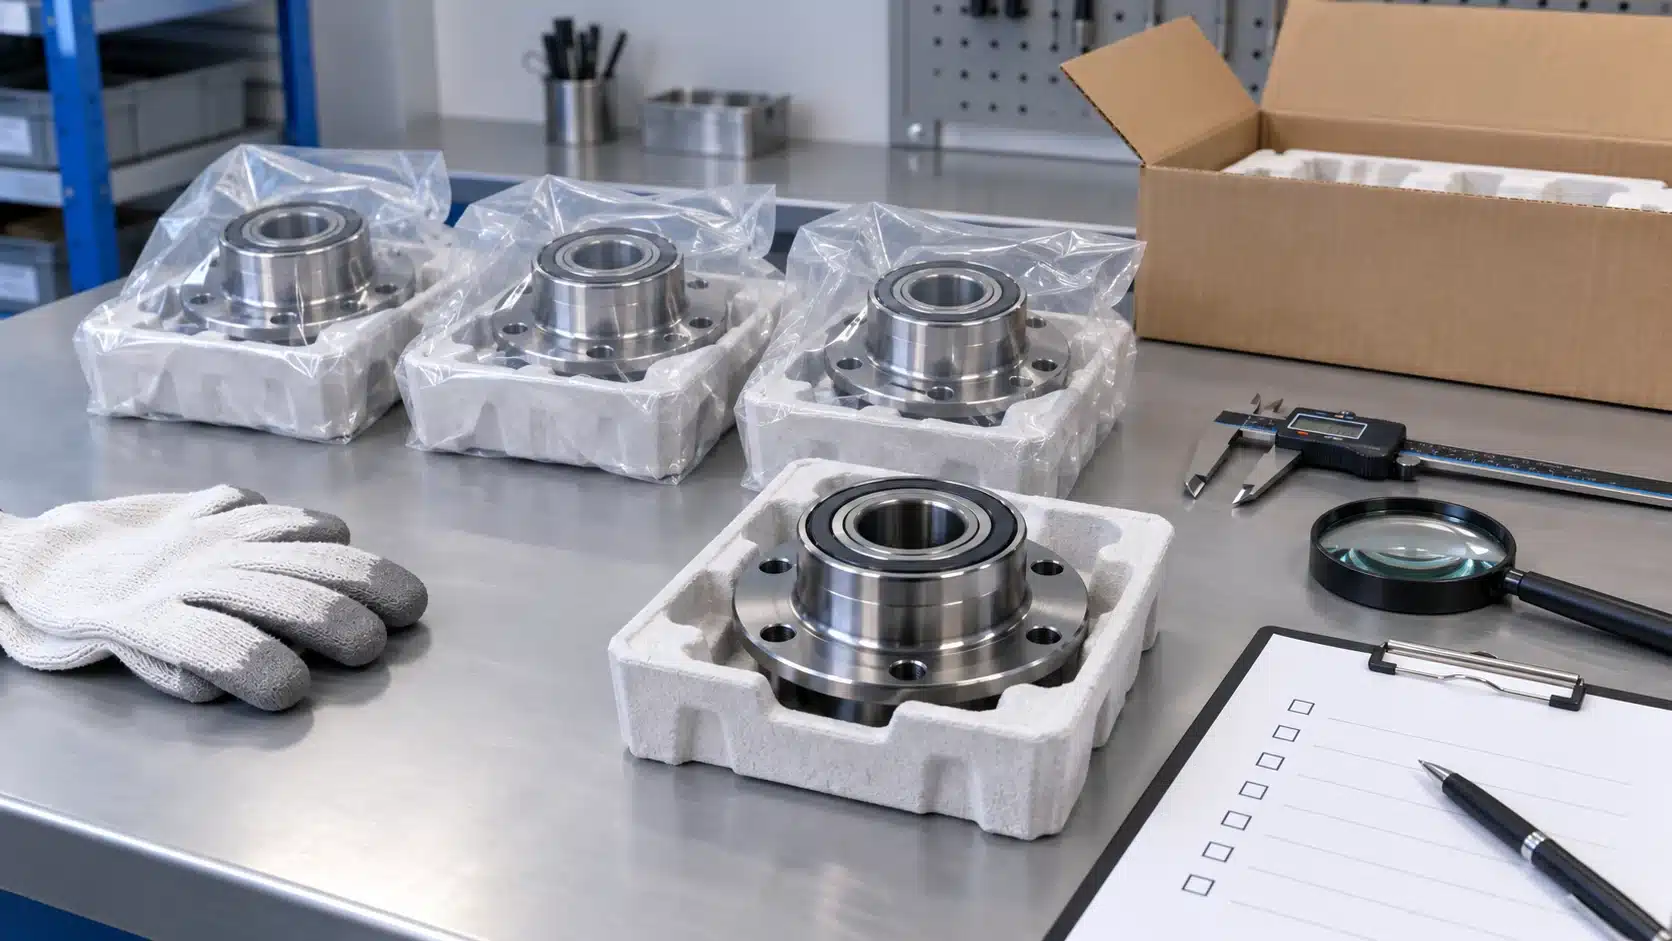
Inspection should address visible damage, contamination, protective features and the parts included in the order. Keep those checks linked to the agreed product and packaging definitions. A missing protective cover may be a discrepancy where the approved pack requires one, while a different design may legitimately use another protection method.
Check accessories by reference and quantity, not just by appearance. An assembly supplied with a nut, bolts, circlip or sensor clips should have a defined kit list. A photograph of several loose items can support identification, but it does not establish that the correct hardware is present in every package.
If moisture or corrosion is found, preserve the delivery evidence before cleaning or repacking. The water-ingress investigation guide explains how package condition and handling history help distinguish observations from causal conclusions. Receiving staff should identify and segregate suspect material according to the plan, then request the appropriate technical review.
Agree sampling before the shipment arrives
The sampling approach should reflect the characteristic, product history, process evidence and consequences of a missed defect. A generic sample percentage is not an adequate substitute for a defined plan. Where a recognised sampling standard is used, identify the edition, lot definition, inspection level and other applicable parameters in the agreement.
Separate destructive tests from checks that can be performed on saleable product. Specify how samples will be selected, identified and replaced where relevant. A supplier choosing a convenient demonstration sample and a buyer randomly selecting from the shipment are different activities; the report should describe which occurred.
Sampling does not guarantee that every unexamined unit conforms. Equally, a claim of complete inspection should identify the characteristic inspected on every unit, not imply that every possible property was tested. Ask for precise scope. This allows the buyer to understand the remaining uncertainty and plan receiving controls accordingly.
Write the reaction plan while decisions are still easy
An inspection sheet should state what happens when a check fails or cannot be completed. Identify who stops release, who reviews the result and how suspect product is separated. Define how the affected scope will be assessed using lot and process records. These arrangements are easier to agree before a delivery deadline creates pressure.
Distinguish a repeat measurement from a retest after correction. Record the reason for each additional check and preserve the original result. If a measurement error is established, document the evidence. If the product is reworked or sorted, the reinspection should describe the changed condition and the criteria used for release.
For unresolved identity or application questions, hold the affected line rather than assuming the rest of a similar-looking shipment provides confirmation. A quick written clarification can prevent a much more difficult downstream return. The plan should make it possible to continue unaffected work while keeping the unresolved product clearly controlled.
Ask for reports that can be reviewed efficiently
A useful report starts with the product and inspection scope. It then lists requirements, methods, sample identities, results and disposition. Include the date, responsible function and any deviations from the agreed plan. Refer to supporting files by stable identifiers so that the reader can find the relevant drawing or test record.
Do not treat a management-system certificate as a replacement for product-specific evidence. The Huayuan quality document checklist explains how buyers can distinguish organisational documents, test reports and shipment records. This is a complementary procurement step: technical inspection determines what was checked, while document review confirms what the evidence applies to.
Where confidential details cannot be shared, agree an appropriate evidence format rather than requesting unrelated marketing claims. A redacted report may still show the sample identity, method, requirement and conclusion needed for a decision. Make any omission explicit so the buyer understands the scope of the available evidence.
Use the first delivery to improve the plan
After the first controlled shipment, review the questions that slowed acceptance. Were reference numbers inconsistent? Did the receiving team lack the current drawing? Did a packing change make labels difficult to read? These are specific opportunities to improve the next order, even where no product defect was found.
An illustrative review might reveal that the supplier reported a feature using one drawing label while the buyer used another. The corrective action would be to align the characteristic dictionary and confirm the measurement method. It would not require inventing a new tolerance or adding every possible test to future deliveries.
Track revisions to the inspection plan and explain why they changed. Link new requirements to product changes, customer needs or investigation findings. Retire obsolete forms through the document process while preserving past records. A repeat order should refer to the current agreed plan, not whichever attachment happens to be easiest to find.
For a JNHJDP wheel hub assembly enquiry, send the proposed reference, application and the characteristics requiring evidence. Use the contact page to request an order-specific discussion of available records and inspection requirements. Capability and test scope must be confirmed for the actual project.
Questions about inspection planning
Is a calibration certificate enough to trust a result?
It is one part of the measurement evidence. The method, setup, equipment suitability and relevant uncertainty also matter. Ask how the result was obtained and whether the process can support the intended acceptance decision, especially when a measured value is close to a limit.
Should buyers require every test on every part?
The inspection strategy should be justified by product and process requirements. Some checks may be appropriate for every unit, while others belong to sampling or development approval. Define the scope with competent technical staff instead of choosing an arbitrary universal test list.
What if the drawing and purchase order disagree?
Resolve the discrepancy before release. Preserve both documents, identify the conflicting requirement and obtain the authorised revision or clarification. An inspector should not choose the more convenient requirement without a documented decision.
What makes an inspection plan useful months later?
Clear links between the order, product revision, sample, method and result make the record reusable. Add a documented reaction and approval. Those connections allow a later investigator to understand what was accepted and why, even if the people involved have changed.