Wheel Hub Flange Dimensions and Bolt Patterns: A Verification Guide
Wheel hub flange dimensions describe several interfaces, not one interchangeable size. A bolt pattern identifies the arrangement of wheel fasteners, while pilot diameters, mounting faces, axial distances, splines and sensor features answer different questions. To verify a proposed wheel hub bearing assembly, compare a controlled drawing and application record with measurements taken from defined reference surfaces. A matching wheel bolt pattern is only one part of that comparison.
This guide is for buyers, catalogue teams and inspectors who need to turn a photograph or supplier dimension table into a checkable technical record. It explains what to ask for, how to distinguish similar terms, and how to prevent sample measurements from becoming unsupported fitment claims. It does not provide vehicle-specific dimensions or installation tolerances.
Begin with the two sides of the hub
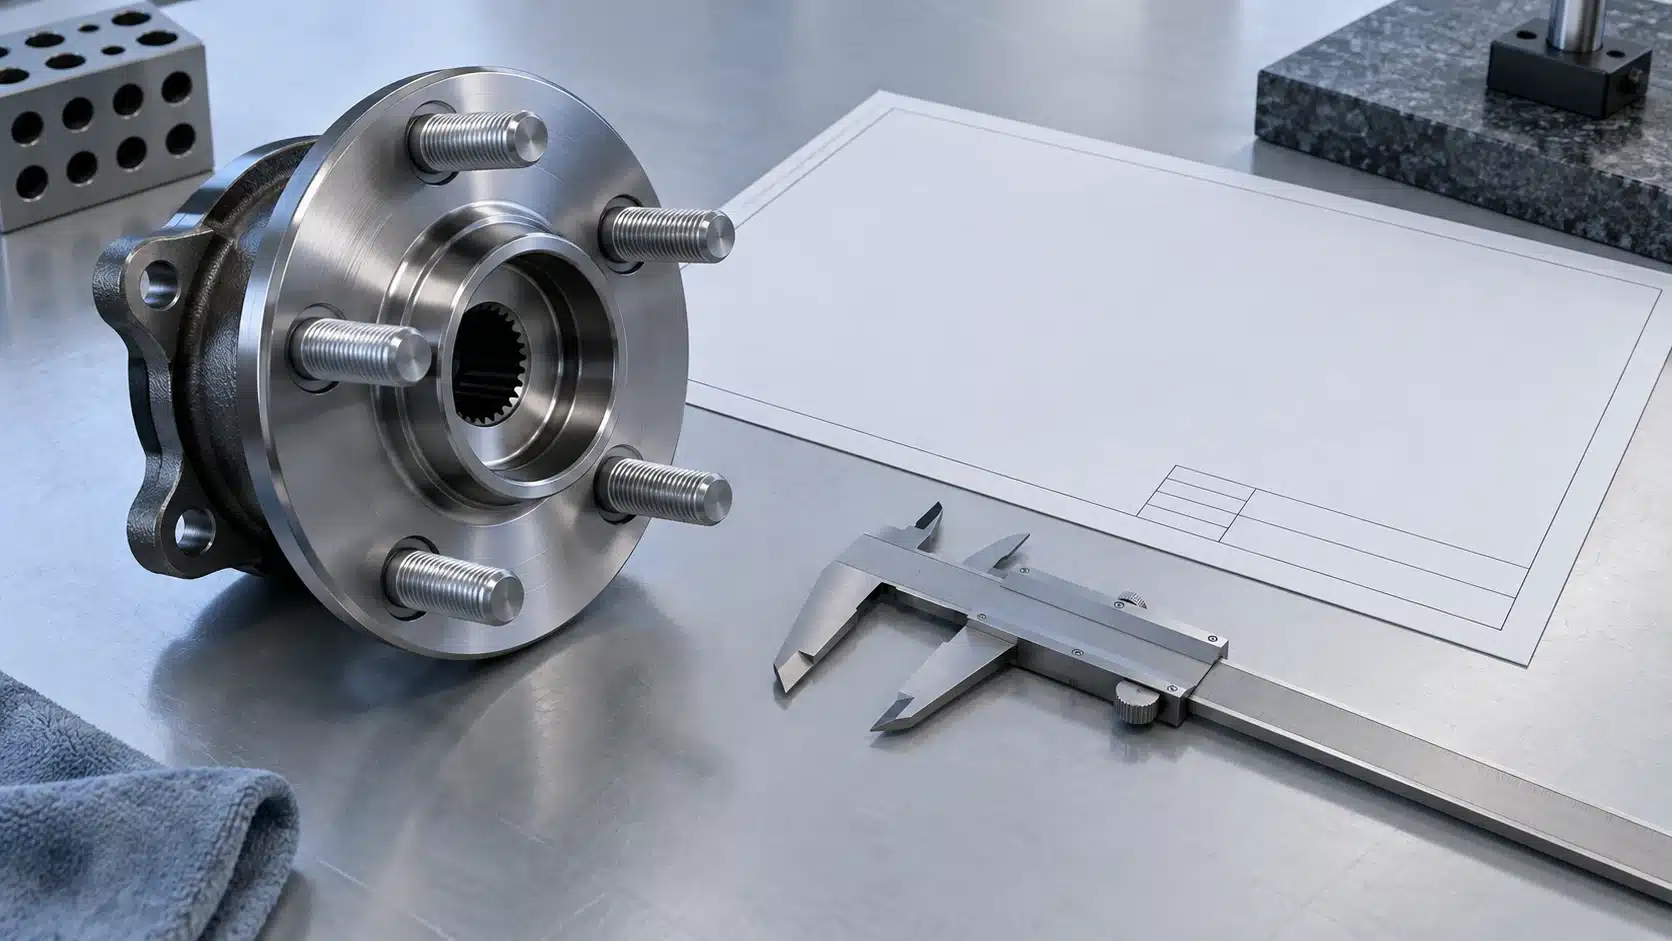
A hub assembly connects rotating components to the wheel-end structure through distinct interfaces. The wheel-side flange and the mounting interface toward the knuckle have different functions. A supplier may call both features a flange, so a spreadsheet column labelled “flange diameter” can be ambiguous even when the number is accurate.
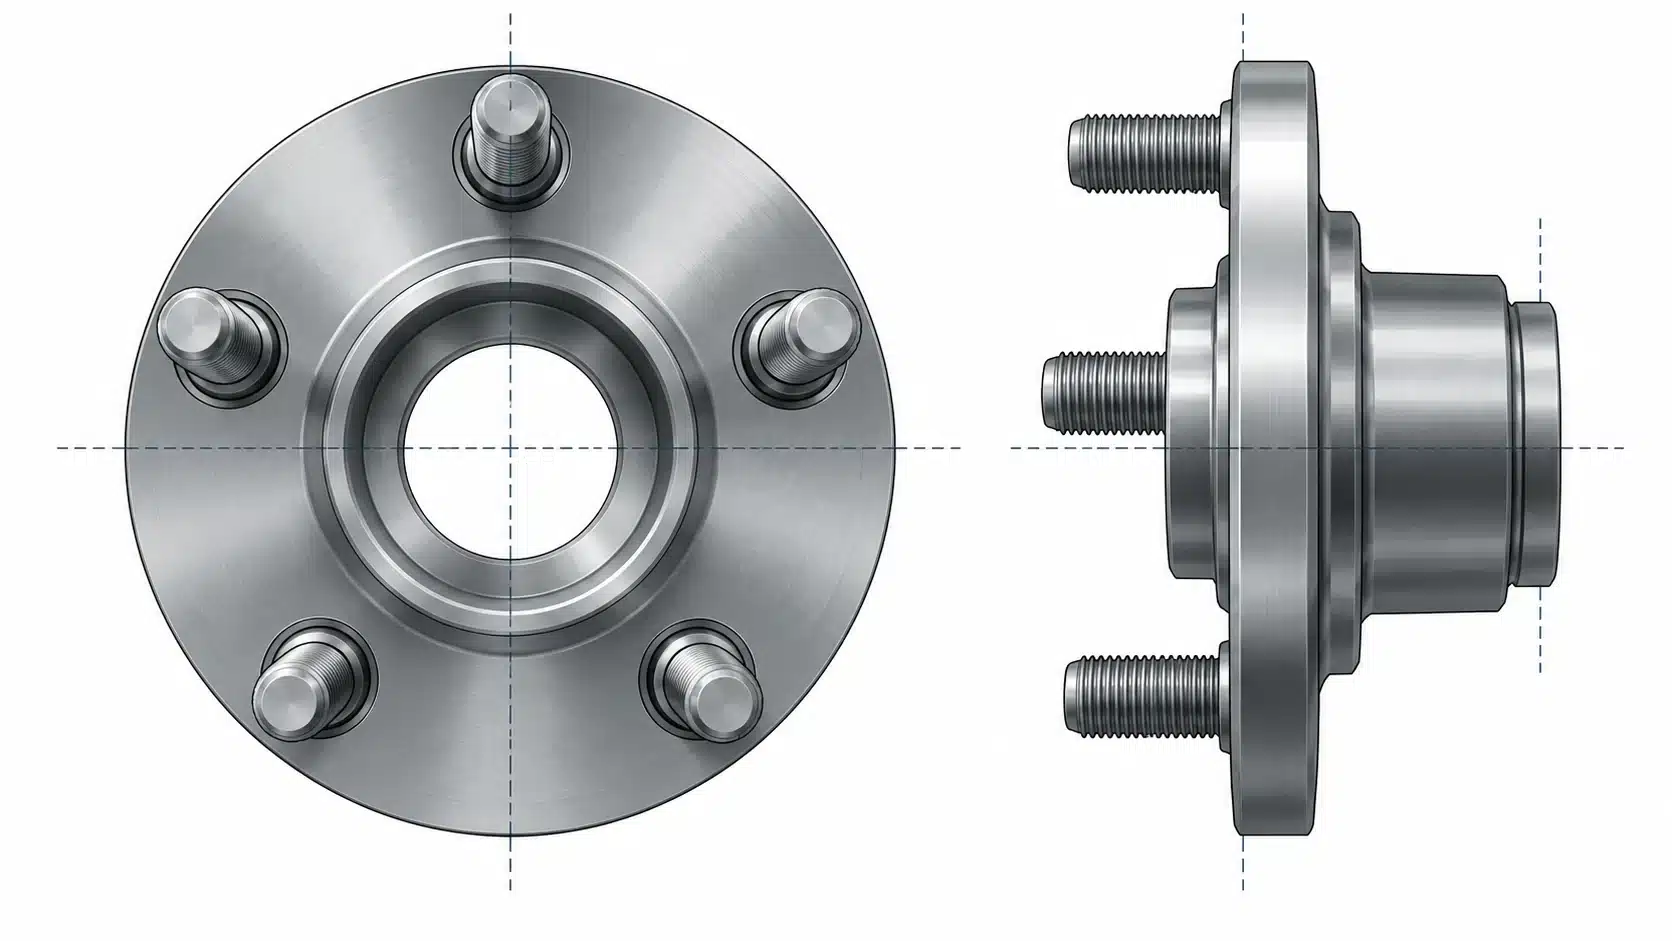
Use an annotated drawing to identify the feature being discussed. Define the wheel mounting face, the relevant pilot surfaces, the bearing axis and the rear mounting face where present. Label any additional shoulders or locating surfaces separately. A simple feature key shared by buyer and supplier is more useful than adding increasingly long descriptions to an unstructured email.
The bearing versus hub assembly guide can help establish which product is being compared. A bearing cartridge, a hub with an integrated flange and a complete assembly may require different records. Determine the product boundary before deciding which measurements belong in the enquiry.
Read a bolt pattern without overinterpreting it
For a conventional evenly spaced circular pattern, a description such as five fastener positions on a specified pitch circle expresses the count and the circle diameter. It does not describe the fastener thread, stud protrusion, seating geometry or the complete mounting relationship. Two parts can share that pattern while differing in other critical features.
Keep the wheel-side bolt pattern separate from the pattern used to attach an assembly to the knuckle. Record whether each position is a clearance hole, threaded hole or installed stud. A photograph can make a through-hole look threaded, especially where shadows or coatings obscure the surface. Request a drawing or a detailed confirmation rather than resolving the uncertainty by appearance.
A catalogue may use millimetres while a workshop note uses inches. Store the original value and unit, then record any conversion in a separate field. Round only according to the purpose of the comparison. A rounded search value is useful for finding candidates, but it should not replace the controlled dimension used for acceptance.
Use geometry only within its assumptions
For an ideal pattern of equally spaced hole centres, the pitch-circle diameter can be related to the chord between adjacent centres. If there are n equally spaced positions and the adjacent centre distance is c, the circle diameter is c divided by sin(180 degrees divided by n). This is a geometric relationship, not a substitute for the drawing or an approved inspection method.
The formula assumes that the measurement represents the centres correctly and that the intended pattern is actually circular and equally spaced. A rough edge-to-edge caliper reading does not necessarily provide c. Hole diameter, stud condition, access and measurement technique can all affect the estimate. For a five-position pattern, simply measuring across two convenient outside edges can therefore produce a misleading result.
Use an approximate result to identify a question, not to approve a safety-relevant interchange. Where the pattern is close to another nominal size, refer the part to a suitable dimensional inspection process. Include the method and uncertainty when interpreting a result near a limit, rather than selecting whichever nominal value looks nearest.
Distinguish pilot diameters from decorative or clearance surfaces
A hub can have more than one cylindrical surface near its centre. The wheel-locating pilot, a brake component locating surface, a bearing seat and a clearance surface should not be merged into one “centre diameter” field. Which surfaces exist and how they function depends on the actual assembly.
Request the axial length and associated shoulder for each relevant pilot, not only its diameter. A short land and a longer land can have the same nominal diameter but interact differently with adjacent parts. Identify chamfers and lead-ins where they affect assembly. A measurement across a chamfer should not be reported as though it were the diameter of the full cylindrical land.
For used samples, document corrosion, coating damage and wear before measuring. A worn part can help establish identity, but its condition can prevent it from representing the original specification. Keep “observed on returned sample” separate from “required by drawing.” That distinction avoids turning service damage into the target dimension for a replacement.
Define height, offset and mounting faces explicitly
Terms such as total height, flange height and offset are often used inconsistently between suppliers. Ask which two surfaces define the distance. A small drawing with two highlighted faces can settle a disagreement that several emails of numbers cannot. Record the direction of measurement and the unit with the value.
Do not substitute wheel offset terminology for a hub assembly’s drawing dimensions. A wheel’s offset and the axial spacing between hub faces are related to different component definitions. Keep the terminology associated with the relevant drawing. If a catalogue offers only “height,” treat it as incomplete until the reference surfaces are identified.
This is also where the bearing axis becomes important. An axial distance is not the same thing as face runout, flatness or perpendicularity. Those properties require their own specification and measurement setup. Reporting a height value does not demonstrate that a flange runs true when the assembly rotates.
Add splines, fasteners and sensing features
For a driven assembly, a spline count alone is an incomplete description of the axle interface. Request the applicable spline specification and reference dimensions through the responsible technical contact. Do not assume that two equally counted spline profiles are interchangeable. A proposed substitution should remain visible in the approval record until the interface is confirmed.
Fastener details also belong in the comparison. Record the specified thread, the relevant length or protrusion, and whether hardware is included. Identify any requirement to use new hardware from the applicable service information. Purchasing should not invent a universal tightening value or reuse rule from the shape of the fastener.
Finally, compare the wheel-speed sensing arrangement. The ABS encoder specification guide explains why the target, sensor and orientation need independent confirmation. Mechanical drawings and sensing records should refer to the same product revision. A correct flange and an incorrect encoder still leave an unsuitable candidate.
Build a dimension dictionary before the spreadsheet grows
The best time to standardise fields is before hundreds of references are imported. Define what each field means, its unit, the permitted source and the expected evidence. For example, “wheel mounting face to rear mounting face” communicates more than “H.” If a drawing uses lettered dimensions, retain those labels but attach the drawing revision.
| Field group | Information to preserve | Common ambiguity |
|---|---|---|
| Identity | Buyer reference, supplier reference, revision | A search alias becomes the order reference |
| Wheel-side pattern | Count, pitch circle and fastener type | Wheel and knuckle patterns mixed together |
| Pilot surfaces | Diameter, land length and location | One centre diameter used for several surfaces |
| Axial geometry | Named start face and end face | Height and offset treated as synonyms |
| Driven interface | Applicable spline definition | Tooth count treated as complete compatibility |
| Sensing | Target and sensor arrangement | ABS noted without configuration |
| Measurement | Method, result, unit and date | Measured sample value replaces specification |
Separate the nominal requirement, permitted limits and measured result. A single cell containing “approximately correct” cannot support inspection or a later dispute. If the requirement is unavailable, mark it as unresolved and assign responsibility for obtaining it. Avoid entering zero for a dimension that was never supplied or measured.
Use a measurement plan that can be repeated
Before taking readings, confirm the sample identity and condition. Clean only according to a method appropriate to the part and the purpose of the examination. If the item is a return under investigation, preserve relevant residues and photographs before any cleaning. Decide whether the activity is identification, acceptance inspection or failure analysis; each has different evidence needs.
The inspector should select equipment and fixturing suitable for the feature and tolerance. A caliper is useful for many preliminary checks, but it does not automatically resolve close fits, runout or complex geometric relationships. Define contact locations, support conditions and the number of observations needed to detect an inconsistent setup.
NIST explains that metrological traceability concerns a measurement result and its documented relationship to references, including uncertainty. A calibration sticker alone does not explain whether a particular hub measurement is fit for its intended decision. For procurement, request enough method information to understand the result rather than simply asking whether the instrument is calibrated.
Where results disagree, compare methods before declaring a supplier error. Ask whether the same features, units, temperature conditions and datum references were used. Repeat the disputed measurement with an agreed setup. Preserve both original results, the reason for the follow-up and the final disposition so that an apparent discrepancy is not hidden by overwriting a spreadsheet cell.
Connect dimensions to application evidence
Dimensional agreement supports a comparison, but it does not independently prove that a hub is suitable for a particular vehicle. Application approval may also depend on load requirements, sensing, hardware and the manufacturer’s intended use. Keep the source of each fitment statement attached to the proposed reference.
The Huayuan OE and fitment verification workflow complements dimensional inspection by organising original references, vehicle variants and unresolved differences. It is useful when a purchasing team must decide which evidence is still missing after the drawing comparison. A catalogue match remains a candidate until the required checks are completed.
Installation information provides another boundary. Timken’s hub unit installation guidance directs users to vehicle-specific requirements. Consequently, a dimension table should not be presented as a fitting procedure or as permission to force a part into an interface that does not match.
Work through a disagreement without guessing
Consider an illustrative purchasing case: two suppliers propose a hub with the same wheel-side bolt pattern, but their tables list different heights. The first task is to check the height definition. One table may include a projecting pilot while the other measures between mounting faces. If both use the same definition, the difference may be substantive and requires technical review.
The buyer should request the current drawings, identify the corresponding faces and preserve the original quotation lines. The next action might be a clarified dimension, a controlled sample measurement or rejection of the candidate. The outcome should not be determined by which supplier responds more confidently or provides the more polished product image.
This example is a workflow illustration, not a claim that any listed JNHJDP part has those differences. Real comparisons need actual references and authorised data. Keeping illustrative cases separate from product claims helps readers apply the method without accidentally importing fictional specifications into their catalogues.
Keep the approved comparison useful for repeat orders
Once a candidate is accepted, retain the drawing revision, measurement report, application source and any agreed exceptions together. Tie them to the purchase-order reference and sample identity. A later order should use that controlled package, not a saved image whose origin and revision are unknown.
Ask how the supplier will communicate changes affecting interfaces, materials, sensing or included hardware. A change does not automatically make a product unacceptable, but it can invalidate an earlier comparison. Define which changes require a new sample or an engineering review, and identify the person authorised to close the review.
Use the wheel hub bearing inspection plan to decide how dimensional requirements become receiving checks. When enquiring about JNHJDP hub assemblies, include the original reference and the particular features needing confirmation. Use the JNHJDP contact page to send the reference, application, drawing revision and open question for review. A focused drawing question produces a more useful response than a request for “all hub sizes.”
Practical questions about hub measurements
Does the same bolt pattern prove interchangeability?
No. It describes only a portion of the interface. Compare the relevant pilots, axial geometry, mounting arrangement, driven interface and sensing system, then verify the intended application. Keep each comparison linked to a source instead of treating one matching value as approval.
Can a used sample define the manufacturing drawing?
A used sample can provide identification clues and observed measurements. Wear, corrosion, deformation and previous repairs may affect it. Any attempt to derive a new specification from a sample requires appropriate engineering work and should be clearly distinguished from checking against an existing approved drawing.
Should every catalogue include complete tolerances?
A public catalogue and an inspection specification serve different readers. The catalogue should present accurate identifying information without implying that omitted details are irrelevant. Obtain the controlled tolerances and methods needed for acceptance through the technical approval process.
What should be sent with a dimensional question?
Provide the reference, drawing revision, annotated feature, original value and unit, measured result, method and sample condition. Include a photograph that shows the measurement location. This gives the technical team enough context to resolve the discrepancy without guessing what “diameter” or “height” meant.